How Steel Assembly Works: From Shop to Site
The steel assembly process moves from shop fabrication to site erection. It combines prefabrication, connection design, and careful sequencing. Understanding these steps helps buyers manage risk, cost, and quality on steel structure projects.
- Shop fabrication controls fit, tolerances, and material handling before components ever reach the site.
- Connection types drive erection speed, inspection effort, and long-term maintenance access.
- Prefabrication reduces on-site labor but increases the need for accurate drawings and early coordination.
- Erection sequencing must match connection design, crane access, and weather protection.
- Clear documentation and field verification prevent rework and delays during assembly.
How Shop Fabrication Prepares the Build
The steel assembly process starts in the fabrication shop. Here, raw materials are cut, formed, welded, and inspected into finished components. The shop is where the design becomes physical. A beam is not just a length of steel. It is a profile with flanges, web, holes, stiffeners, and a specific length measured to the millimeter.
Fabricators use shop drawings derived from the structural design. These drawings show every member, its orientation, its connection points, and any field modifications. The shop must account for material tolerances, cutting methods, and welding procedures. If a hole is drilled in the wrong place, the connection will not align. If a member is twisted, it will be difficult to set in the frame.
The shop also handles coating. Paint, thermal spray, or other protective systems are applied in controlled conditions. This is often more efficient than field coating. It reduces exposure to weather and allows for thicker, more durable protection. Coating systems affect maintenance intervals and the long-term performance of the structure.
Buyers should treat the shop as the first point of quality control. The shop must verify member lengths, hole patterns, and welds against the design. A single error here can travel to site and stop the erection crew. The cost of fixing a fabrication mistake is often higher than catching it in the shop.
How Prefabrication Changes the Sequence
Prefabrication means building as much of the structure in the shop as possible. This can include complete bays, roof trusses, purlins, and bracing. The goal is to reduce on-site work. Instead of welding and bolting on site, the crew receives members that are ready to connect.
Prefabrication affects sourcing decisions. A heavily prefabricated project may require fewer site welders but more precise crane capacity. It may also require a larger laydown area to stage completed bays. The shop must plan for transport limits. A long truss may not fit on a standard truck. It may need a special permit or a different transport method.
There are trade-offs. Prefabrication saves site time but increases the need for accurate drawings. If the shop and the site engineer disagree on a detail, the error will show up during erection. The site may have to cut, modify, or replace a member. That causes delay and waste.
A good prefabrication plan includes a clear cut list, a shop drawing review, and a mock-up of critical connections. The buyer should ask how the shop verifies the fit of major connections. The answer should include physical checks, not just visual review.
How Connection Types Affect Erection
Connection types determine how members join. The most common types are bolted, welded, and hybrid. Bolted connections are fast to install. They allow for adjustment and are easier to inspect. Welded connections are strong and compact. They reduce the number of field operations but require skilled welders and inspection.
Bolted connections come in different forms. Moment connections transfer bending. Shear connections resist lateral force. Some connections use high-strength bolts that require torque control. Others use standard bolts. The choice affects the number of bolts, the size of the plates, and the time needed per joint.
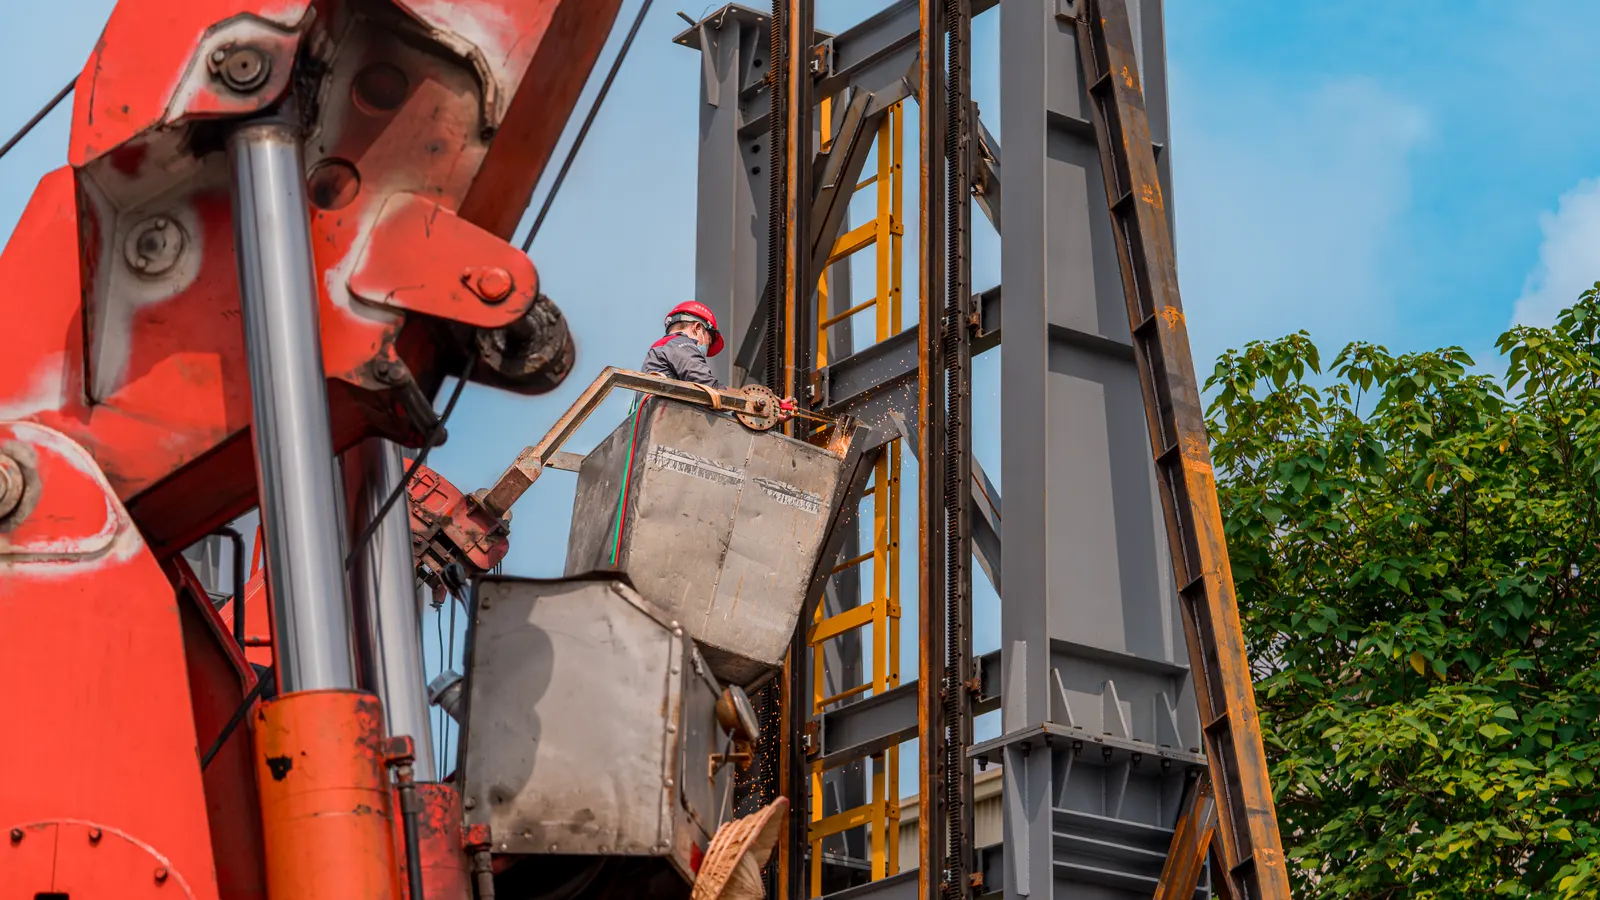
Welded connections require access for the welder. The joint must be clean, dry, and within temperature limits. In cold or wet weather, field welding can be difficult. Coatings can also interfere. Welding on a coated member may require grinding and recoating.
Hybrid connections combine bolts and welds. This can reduce field work while keeping some of the benefits of each method. The decision depends on the project. A long-span warehouse may use bolted connections for speed. A heavy industrial building may use welded or hybrid connections for stiffness.
The buyer should consider maintenance access. A connection that is hard to reach may be difficult to inspect or repair. A connection that is exposed to corrosion may need more protection. The connection type is not just a structural choice. It is a lifecycle choice.
How the Erection Crew Assembles the Frame
Site erection starts with foundations. The steel base plates sit on concrete pads. The pads must be level and at the correct height. If the foundation is out of tolerance, the steel will not sit correctly. The crew may need shims or adjustments.
The first column goes up. Then the beams. Then the bracing. The sequence is usually vertical first, then horizontal. This gives the frame stability. Temporary bracing may be used until permanent bracing is installed. The frame must be plumb and square before moving to the next bay.
Crane access is a major factor. The crane must be able to reach every connection point. The operator must have a clear line of sight. The ground must be firm. If the crane cannot reach a high connection, the crew may need a different lift plan. This can slow the schedule.
The erection crew uses a plan that matches the connection type. Bolted connections are tightened to specification. Welded connections are inspected. The crew records torque values, welder qualifications, and inspection results. These records support the owner and the inspector.
A common mistake is rushing the sequence. The crew wants to finish the bay. They may skip a check. The next member does not fit. The whole bay is reworked. The schedule slips. A disciplined sequence prevents this.
How Documentation and Coordination Reduce Rework
The steel assembly process depends on documentation. The site needs the shop drawings, the erection sequence, the connection details, and the quality plan. The site engineer must be able to find the answer to a question quickly.
The shop and the site must communicate. If a member arrives and does not match the drawing, the site engineer must know who to call. If a connection is difficult to access, the engineer must know whether the shop can modify it. If a foundation is out of tolerance, the engineer must know what adjustments are allowed.
The buyer should require a single point of contact. This could be the site engineer or the project manager. That person must have the authority to make decisions. Without it, the crew waits. The crane idles. The schedule slips.
A good coordination meeting happens before erection starts. The crew reviews the sequence. The engineer reviews the drawings. The buyer reviews the risks. The meeting produces a clear plan. The plan is not just a list. It is a set of decisions.
How Quality Checks Protect the Final Structure
Quality checks happen at every stage. The shop checks the members. The site checks the foundations. The inspector checks the connections. The owner checks the final result.
The shop may use visual inspection, dimensional checks, and non-destructive testing. Welds may be checked with dye penetrant or ultrasonic testing. The site may check plumb, level, and alignment. The inspector may check bolt torque and weld quality.
The buyer should define the acceptance criteria. What is the maximum deviation for a foundation? What is the minimum torque for a bolt? What is the inspection level for a weld? These criteria must be in the contract. Without them, there is no standard to hold the contractor to.
A final inspection is not just a formality. It verifies that the structure is complete and safe. It checks for missing bolts, damaged coatings, and loose connections. It confirms that the as-built drawings match the installed structure.
The steel assembly process is a chain. Each link depends on the one before it. A strong connection in the shop is useless if the site cannot install it. A perfect foundation is useless if the steel does not fit. The buyer must manage the whole chain.
How a Typical Project Flows From Shop to Site
A typical project starts with a design. The design is developed by an engineer. The engineer chooses the members, the connections, and the sequence. The design is then sent to the fabricator.
The fabricator creates shop drawings. These drawings are reviewed by the engineer and the buyer. The fabricator cuts, forms, welds, and coats the members. The members are inspected and staged. They are loaded onto trucks and shipped to site.
At site, the foundations are prepared. The crew sets the first column. The crew sets the beams. The crew sets the bracing. The crew tightens the bolts and inspects the welds. The crew moves to the next bay.
The project continues until the frame is complete. Then the roof, cladding, and other elements are installed. The final inspection is performed. The as-built drawings are updated. The project is handed over.
This flow is the steel assembly process. It is not a single event. It is a series of decisions and checks. The buyer must understand each step. The buyer must ask the right questions. The buyer must manage the coordination. The result is a structure that works as intended.
Frequently asked questions
What is the main benefit of prefabrication in steel construction?
Prefabrication reduces on-site labor and weather exposure. It also improves fit and quality because work is done in a controlled shop environment.
How do connection types affect the erection schedule?
Bolted connections are usually faster to install but require careful torque control. Welded connections can be slower but reduce the number of field operations.
What documents should the site engineer review before erection starts?
The engineer should review shop drawings, the erection sequence, connection details, and the quality plan. These documents ensure the crew knows what to install and how.
Why is crane access important during steel erection?
Crane access determines how members can be lifted and set. If the crane cannot reach a connection point, the crew may need a different lift plan, which can delay the schedule.
How does the buyer control quality during the steel assembly process?
The buyer defines acceptance criteria in the contract. The buyer requires documentation and inspections at the shop and site. The buyer uses a single point of contact to manage decisions.